Monthly Archives

October 2026

Customer engagement does not always require a massive video wall. For many retail stores, corporate spaces, galleries, hospitality venues, and other commercial environments, a strategically positioned small LED screen display can communicate information at the exact point where customers make decisions. Its value comes from combining visual impact with proximity, relevance, and flexible content, turning otherwise overlooked spaces into useful communication opportunities.


Why Smaller Displays Can Create Bigger Engagement Opportunities


Large screens naturally attract attention, but size is only one factor in effective digital communication. A smaller display can be placed closer to products, reception desks, counters, shelves, or customer waiting areas, allowing businesses to deliver information when it is most relevant. Samsung’s retail guidance similarly highlights smaller displays positioned around merchandising shelves and tables as tools for product information and digital headers.


This proximity changes how customers interact with content. Instead of simply noticing a large advertisement from a distance, a customer standing near a product can see detailed information, promotional messaging, demonstrations, or complementary recommendations. A micro LED display can therefore serve a more focused role within the customer journey rather than competing for attention across an entire room.


A Small LED Screen Display Can Guide Decisions


Customer engagement is closely connected to useful information. Digital signage can answer questions before customers need to ask an employee, provide additional product details, and guide visitors toward relevant services. This is particularly useful in environments where customers may spend several minutes browsing or waiting.


A small LED screen display can highlight specifications, explain product benefits, promote limited-time offers, or introduce related products. Content can also be changed according to time, season, inventory, or promotional campaigns. Such flexibility helps businesses keep communication current instead of relying on printed materials that become outdated.


Close Viewing Makes Image Quality More Important


Small-format displays are often installed where viewers stand relatively close to the screen. That makes image clarity particularly important. Coarse pixel structures that appear acceptable from a distance may become more noticeable when customers are only a few meters—or less—from the display.


A fine-pitch micro LED display can address this requirement by providing a denser visual structure suited to close viewing. For premium corporate environments, studios, control rooms, and luxury retail spaces, visual consistency can influence how customers perceive the overall quality of the brand environment.


Content Should Match the Customer’s Context


Hardware alone does not create engagement. The message displayed, its timing, and its relationship to the surrounding environment determine whether customers pay attention. Digital signage can combine images, text, video, promotions, and educational content, allowing businesses to create more relevant communication at different points in the customer journey.


For example, a retailer could use a display near a product category to explain key features, while a hotel might promote dining or wellness services near its reception area. A corporate lobby could use a micro LED display for brand storytelling, company information, event announcements, or welcome messages. Each application gives the screen a specific purpose rather than making it another generic advertising surface.


Brightness Matters in Commercial Environments


Ambient lighting can significantly influence display visibility. A screen positioned near windows, in a brightly illuminated lobby, or under strong indoor lighting needs sufficient brightness to maintain visual impact without producing distracting glare.


The Coblinks CM-S Series is designed for premium indoor fixed installations and uses semi-outdoor brightness levels to address strong ambient light. This makes the series suitable for environments such as brightly lit lobbies, galleries, and sunlit retail spaces where maintaining vibrant visuals can be challenging.


Precision and Slim Design Support Premium Spaces


Physical integration also affects customer perception. A display that dominates its surroundings or requires excessive installation depth can conflict with carefully designed commercial interiors. Slimmer hardware can make digital content easier to integrate into architectural environments while preserving visual prominence.


The Coblinks CM-S Series has a 41mm slim profile and offers pixel pitches from 0.9mm to 1.8mm. Its 4-in-1 technology is designed to produce a smoother, more coherent image with reduced graininess, making it particularly relevant to close-viewing applications such as boardrooms, studios, and control rooms.


Turning Digital Signage Into a Customer Touchpoint


Businesses can gain more from a small LED screen display when it is treated as part of a broader engagement strategy. Content management, placement, customer behavior, and campaign objectives should be considered together. Digital signage can support promotions, education, wayfinding, product discovery, and brand communication rather than being limited to advertising.


This also makes measurement possible. Businesses can compare customer traffic, dwell time, conversions, or campaign responses around different display locations. Current digital-signage guidance recommends defining objectives, auditing the physical site, planning content, and considering scalability before deployment.


Coblinks CM-S Series for Close-Viewing Applications


Coblinks is a technology-driven LED display manufacturer specializing in indoor and outdoor fixed-installation and rental displays, supported by complete SMT production lines and advanced manufacturing equipment. Its CM-S Series is positioned as a professional micro LED display for premium indoor fixed installations.


With 0.9mm to 1.8mm pixel pitches, a 41mm slim profile, 4-in-1 technology, and semi-outdoor brightness levels, the CM-S Series is designed for applications where visual precision and environmental integration matter. It can serve corporate lobbies, broadcast studios, command centers, galleries, and retail spaces that demand high-quality close-range visuals.


Making Every Display Space More Valuable


Small displays can make customer communication more precise because they place relevant content closer to the people who need it. A well-positioned micro LED display can support product education, promotions, brand storytelling, and service information, while a small LED screen display can transform shelves, counters, lobbies, and waiting areas into active engagement points.


Coblinks provides professional LED display solutions for businesses seeking high-quality visual communication and customized applications. Companies planning premium indoor installations can contact Coblinks to discuss the CM-S Series and select a display configuration suited to their viewing distance, ambient-light conditions, installation environment, and customer engagement objectives.
0 comment
0 FacebookTwitterPinterestEmail

A new mountain-bike shoe can feel wrong for several different reasons, and treating every problem as a simple size error often hides the real cause. Pressure at the toes may come from insufficient length or a compact toe box; numbness over the top of the foot can involve instep volume or closure tension; heel movement can reflect retention geometry; and discomfort around the pedal can be connected to cleat compatibility or foot position rather than the last itself.


Troubleshooting works best when symptoms are separated by location and then traced back to measurable dimensions or shoe structure. The starting point is therefore not a guess about whether a rider “needs one size up.” It is a comparison between foot length, foot width, toe-box volume, instep space, heel retention, and the intended pedal system.


Measure the Foot Before Blaming the Size Label

Measurement establishes whether the basic dimensions are plausible before any adjustment to closure or cleat position. A practical method for how to measure foot length places a sheet of paper against a wall, has the rider stand with the heel lightly touching the wall, marks the longest toe, and measures the distance from the wall edge to that mark.


Because left and right feet can differ, the sizing baseline can be based on the longer foot. Width is checked separately while standing by marking the widest points of the forefoot and measuring between them. Those two dimensions are more informative than an EU number alone because different models can use different lasts and internal volumes. Triathlon shoes may carry the same printed size while using a different opening, upper volume, and retention geometry.


Size Numbers Do Not Define Shoe Shape

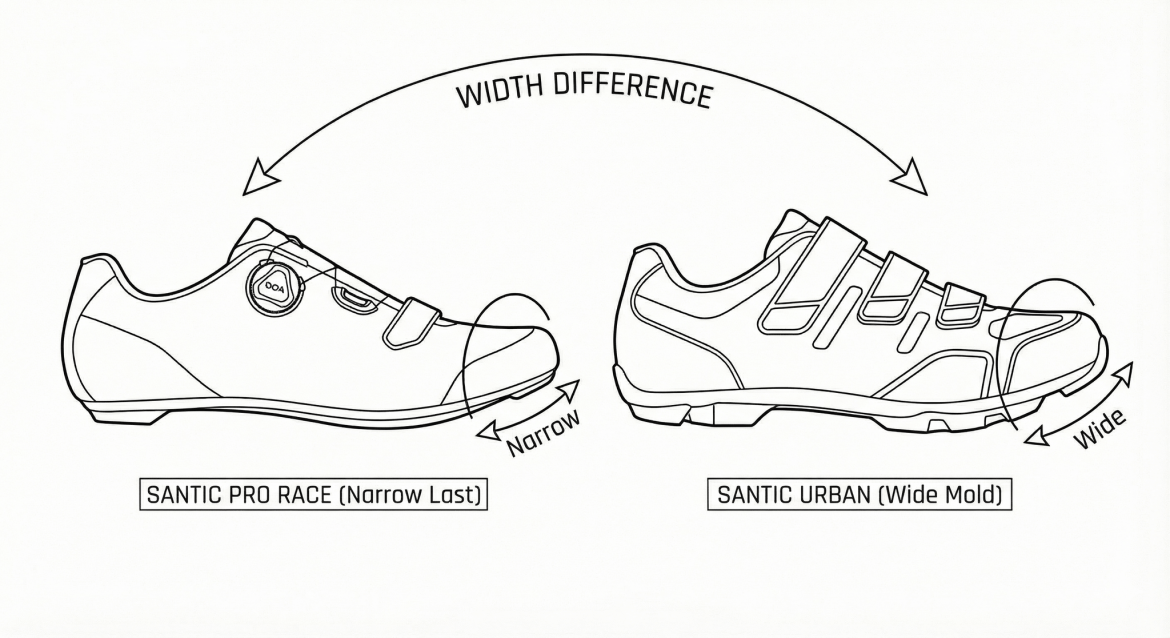
The same printed size can fit differently in an MTB model and in triathlon shoes because their entry and retention structures serve another riding context. A triathlon model may use a wide entry opening and transition-oriented closure, while a Pro Race MTB design may use a more compact last and a highly rigid sole.


Fit troubleshooting therefore begins by separating “size” from “shape.” If measured length is appropriate but the forefoot feels compressed, width or toe-box volume deserves attention. If the forefoot is comfortable but the heel lifts, the problem lies elsewhere. Symptom location points toward the part of the shoe that governs that area. The procedure for how to measure foot length confirms the longitudinal dimension before those shape differences are assessed.


Match the Symptom to Volume, Retention, and Structure

Pressure over the top of the foot points to a different variable than toe clearance. Knowing how to measure foot length remains useful, but tightness or numbness on the instep may indicate that the shoe’s upper volume or closure position is not well matched to a higher instep.


Four- and five-star instep-adjustability ratings correspond to upper volume and dial placement configured to accommodate a higher instep with fewer concentrated pressure points. Toe-box space, forefoot width, and heel containment should be considered independently, because loosening a closure to relieve one area may create movement in another.


Triathlon shoes show a different way of managing entry and retention. Santic’s NF model uses a wide opening, quick hook-and-loop entry, 3D mesh, outsole ventilation, and an EVA insole so the foot can enter quickly after the swim and still be supported during the bike leg.


An MTB shoe used over rough ground may place more emphasis on a secure heel, protective upper, and controlled forefoot position. The contrast shows that fit is not a universal sensation produced by size alone; it results from the last, upper, closure, insole, heel structure, and intended riding movement working together.


Check the Pedal Interface After Basic Fit Is Confirmed

Pedal-interface checks belong later in the diagnostic sequence. After foot length and width have been measured to establish the basic dimensional fit, new MTB footwear also has to match the chosen pedal and cleat arrangement.


Santic’s Alps model uses a full-carbon outsole with stiffness index 14, an EVA cushioned insole, TPU/microfiber/mesh upper, laser ventilation, TPU toe protection, replaceable forefoot spikes, and MTB cleat compatibility in 2- or 4-bolt formats including SPD. A highly rigid sole can make small positioning differences more noticeable because the platform itself does not deform much around the foot.


That is another reason triathlon shoes cannot be used as a direct fit reference for every MTB model. Their closure speed, upper ventilation, sole stiffness, and cleat environment can differ substantially. A rider who feels forefoot pressure only after clipping in may need to distinguish shoe volume from pedal-interface position; a rider who feels heel movement while walking may need to examine retention rather than cleat choice.


The most useful troubleshooting order is measurable fit first, localized pressure second, heel and closure behavior third, and pedal compatibility after those variables are understood. That sequence prevents one symptom from being blamed on the wrong part of the system.


Fit problems in new MTB footwear become easier to solve when they are treated as separate mechanical questions instead of one vague sizing complaint. Length and width establish the dimensional baseline, toe-box and instep volume explain many pressure patterns, heel structures and closures control internal movement, and the cleat interface adds another variable once the shoe is on the bike.


Santic’s sizing method and model differences make that hierarchy visible. A nominal size can start the process, but it cannot finish it. The final fit depends on where the foot needs room, where it needs restraint, and how securely the shoe connects that foot to the selected pedal system. A measured, symptom-by-symptom sequence also avoids unnecessary changes to a shoe that may already be correct in several other dimensions.

0 comment
0 FacebookTwitterPinterestEmail

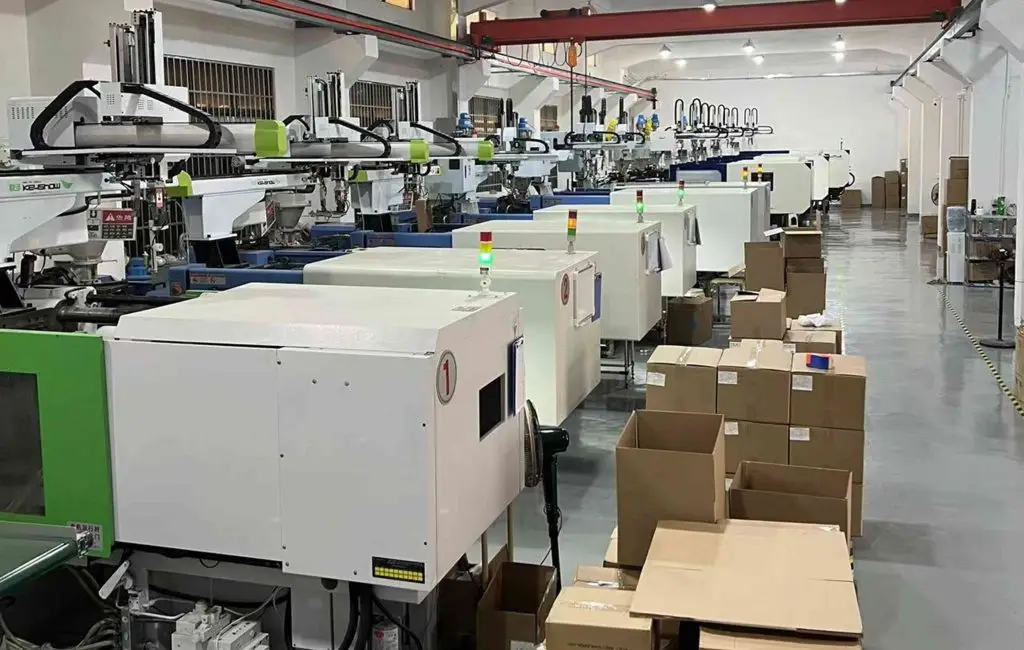
The right electronics supplier should match the needs of the product, not just the target price. When companies compare China electronics manufacturers, they should look at engineering support, prototype capability, production scope, quality processes, communication, and flexibility. These factors can affect development time and production results long after the initial quotation has been accepted.


The selection process should also reflect the product’s current stage. A new concept may need design support and prototypes, while a tested product may need stable assembly and larger production capacity. Knowing these differences makes supplier comparisons more practical.


Define the Project Before Contacting Suppliers

A clear project brief gives manufacturers the information they need to assess a product. It can include product functions, estimated dimensions, expected quantity, target market, and development stage.


Technical documents are also useful. Depending on the project, a supplier may need schematics, PCB files, BOMs, drawings, firmware requirements, or prototype samples.


Without clear requirements, quotations from different manufacturers can be difficult to compare. One supplier may include engineering work, while another may quote production only.


What Engineering Support Is Available?

Engineering support matters when a product is still being developed. A design that works in testing may require changes before it is suitable for repeated manufacturing.

Companies should ask whether the supplier provides DFM evaluation, PCB-related engineering, structural support, or other development services. They should also understand when engineers become involved in the project.


For startups and design firms, this support can be useful when internal engineering resources are limited. It can also help established companies manage a new product without creating a separate manufacturing engineering team.


Prototype Capability Shows More Than a Sample

A prototype allows engineers to examine the actual product rather than relying only on drawings or simulations. It can reveal problems with dimensions, component placement, assembly, or product functionality.


Rapid prototyping is useful when a project needs several design revisions. Each version can provide feedback before the product moves toward larger production quantities.


When comparing suppliers, companies should ask how prototype changes are documented and how the results are transferred into production. This helps connect early development work with later manufacturing requirements.


Compare the Full Production Scope

Price comparisons become more meaningful when the scope of service is clear. A supplier may provide PCBA production only, while another may also handle enclosure manufacturing, assembly, testing, and packaging.


Companies should identify which processes are included in the quotation. Tooling, component sourcing, testing, and packaging may need separate consideration depending on the project.


A broader manufacturing scope can also reduce the number of separate suppliers involved. This may simplify communication when a product contains both electronic and mechanical components.


Does Production Flexibility Match Demand?

Production volume can change during a product’s lifecycle. A project may begin with prototypes, move to a small trial run, and increase production after market feedback.


For this reason, companies should discuss production flexibility before selecting a supplier. The manufacturer should understand the expected development path rather than only the first order.


No MOQ requirements may also be relevant to early-stage projects. Smaller quantities can give businesses more room to test a product before making larger production commitments.


How Should Quality Control Be Evaluated?

Quality control should cover the complete production process. PCB assembly, enclosure manufacturing, final assembly, and product testing can each affect the finished unit.


Companies can ask how incoming materials are checked, how assembly quality is inspected, and what testing is performed before shipment. They can also ask how production problems are recorded and addressed.


Clear quality procedures are especially important for products with several components and manufacturing stages. A supplier should be able to explain its process in terms that the customer can review and understand.


Communication Can Affect Project Results

Supplier communication is easy to overlook during the initial selection process. It becomes much more important once engineering changes or production issues appear.


Companies should identify who will handle technical questions, sample approvals, production updates, and quality discussions. A clear communication process can reduce delays when specifications change.


Document control also matters. BOM revisions, drawings, firmware versions, and test requirements should be tracked carefully so that different teams are working from the same information.


A Practical Example of Supplier Scope

A company that needs development and manufacturing under one workflow may look for a supplier with capabilities across several stages. Minewing is based in Shenzhen, China, and has more than 20 years of experience in electronics manufacturing. They support startups and global brands from initial prototyping to mass production.


Their stated services include PCB design, PCBA production, enclosure design and manufacturing, assembly, testing, and packaging. They also offer OEM, ODM, and JDM cooperation models. This combination can be relevant to businesses that need both product development and manufacturing support.


The company also states that its services have no MOQ requirements. For early-stage projects, this can provide another option when production quantities are still being evaluated.


Which Cooperation Model Fits?

The cooperation model should reflect how much development work the customer needs. OEM can be suitable when the customer already has a defined product design and needs manufacturing support.


ODM may be considered when a company needs more assistance with product development. JDM provides another model for projects where the customer and manufacturer share development responsibilities.


Before choosing a model, companies should clarify ownership of designs, engineering responsibilities, revision procedures, production requirements, and communication channels.


Questions to Ask Before Production

A supplier evaluation should end with specific questions rather than a general impression. Companies can ask about prototype lead times, DFM reviews, production capacity, testing, sourcing, quality control, and packaging.


They should also confirm which manufacturing processes are performed internally and which involve outside suppliers. This gives the project team a clearer understanding of the production chain.


For businesses comparing a China electronics manufacturers supplier, these details can provide a stronger basis for evaluation than price alone.


When Should a Supplier Be Reconsidered?

Supplier evaluation does not necessarily end after the first production order. A project may change significantly as quantities increase or new product versions are developed.


A company may need to reassess the supplier if production requirements change, new components are introduced, or additional engineering support becomes necessary. Quality performance and communication should also remain part of the review.


This is particularly relevant for products that are expected to develop over several production cycles. A supplier that fits an early prototype project may have different capabilities from those required for later production.


Choosing Based on Product Fit

Selecting an electronics manufacturer in China is a comparison of capabilities, responsibilities, and project requirements. The quoted unit price is only one part of that assessment.


Minewing provides OEM, ODM, and JDM services alongside product development and manufacturing support. They describe their workflow as covering the path from prototyping to mass production, which may suit businesses looking for connected development and manufacturing services.


For companies researching China electronics manufacturers, a useful final step is to compare suppliers against the same checklist: engineering support, prototype capability, production scope, quality control, communication, flexibility, and commercial terms. A supplier that fits the actual product requirements can make the path from design to production easier to manage.


0 comment
0 FacebookTwitterPinterestEmail

Selecting a rosin ester resin, such as glyceryl rosinate, for an adhesive system involves more than comparing a single specification. Adhesive formulators and raw-material buyers may need to consider the intended application, processing conditions, resin grade, physical form, documentation, and supply arrangements together. A structured selection process can make it easier to narrow down suitable materials before further internal evaluation.


Defining Target Performance Parameters in Early Formulation Stages


The selection process can start with the requirements of the finished adhesive and the conditions under which the material will be processed. Different adhesive applications may place different priorities on properties such as tack, peel behavior, cohesion, or temperature resistance. Defining these requirements first gives purchasing and technical teams a clearer framework for discussing potential rosin ester grades.


Material specifications can then be reviewed against those initial requirements. Depending on the product, technical documentation may include information such as softening point, acid value, color, and other applicable specifications. These figures provide a basic reference for comparing grades, while the final choice should remain consistent with the manufacturer’s own development and approval procedures.


Supplier documentation also has an important role during early screening. A rosin ester resin manufacturer should be able to provide relevant product information so that technical and purchasing teams can understand the characteristics of each available grade. Clear documentation makes supplier discussions more focused and helps buyers distinguish between materials intended for different industrial requirements.


Product selection does not have to begin with a large number of candidates. A practical shortlist can be developed by identifying the most relevant end-use requirements, then comparing the specifications and supply information of available grades. This approach keeps the early sourcing stage organized without assuming that one resin grade will suit every adhesive system.


Matching Resin Softening Points and Viscosity to Processing Equipment


Physical properties become particularly relevant when a selected resin needs to be handled within an established manufacturing process. Softening point and viscosity information can help technical teams understand how different grades may fit within their existing processing conditions. Buyers can review these specifications alongside the operating range and material-handling requirements of their own facilities.


Physical form should also be confirmed before an order is placed. Rosin ester resins may be supplied in solid forms such as flakes, pastilles, or other formats depending on the grade and supplier arrangement. The supplied form can affect storage, feeding, weighing, and material transfer procedures, making it useful to clarify this information during supplier discussions.


Packaging requirements deserve similar attention. Industrial buyers may need to confirm package type, unit weight, labeling, and other delivery details before receiving materials at the plant. Matching the incoming packaging format with existing warehouse procedures can make routine handling more straightforward and reduce avoidable issues during material receiving.


Processing conditions should ultimately be evaluated by the adhesive manufacturer using its own equipment and procedures. Supplier data can provide a starting reference, but internal technical teams remain responsible for determining whether a particular grade fits their production process. Clear communication between the buyer and supplier is therefore useful before regular purchasing begins.


Balancing Elastomer Compatibility and Long-Term Thermal Aging Behavior


Rosin ester resin is used across different adhesive systems, and their suitability can depend on the polymer base and intended application. Formulators may therefore need to discuss the relevant polymer family with a supplier when comparing resin grades. Rather than assuming that one tackifying resin works across all systems, material selection can be approached by matching documented product characteristics with the requirements of the specific adhesive.


Thermal conditions provide another point for discussion. Adhesive manufacturing may involve heating during material processing, so buyers can review applicable temperature-related information when comparing candidate grades. Where long-term thermal exposure is important to the finished product, the manufacturer’s internal evaluation procedures can determine which material is appropriate for the intended application.


Color and other documented physical specifications may also matter in applications where appearance or material consistency is part of the product requirement. These specifications should be reviewed using current supplier documentation rather than relying on general assumptions about a resin category. Keeping the evaluation tied to documented grade information makes technical discussions more precise.


The same principle applies when considering aging-related requirements. Instead of treating a general resin characteristic as a guarantee of finished adhesive performance, formulators can identify the environmental conditions relevant to their application and discuss the available product information with suppliers. Any final performance assessment can then be carried out through the manufacturer’s established development process.


Securing Batch Consistency and Engaging Technical Teams at CHINACOAT 2026


Once a suitable grade has been identified, procurement teams also need to consider whether the supplier can support the intended purchasing pattern. Relevant questions may include available grades, regular order quantities, packaging formats, documentation, expected lead times, and delivery arrangements. These factors become increasingly important when an adhesive producer plans recurring purchases rather than a one-time evaluation.


Supplier communication can also help connect technical requirements with purchasing decisions. Buyers may share the specifications and material information required by their internal approval process, while suppliers can clarify the corresponding product documentation and available supply options. A clear exchange of information gives both sides a practical basis for discussing regular orders.


KOMO provides product information and sourcing support for industrial customers evaluating rosin ester materials. Discussions can cover product grades, specifications, physical forms, packaging, and supply requirements according to the buyer’s needs. For adhesive manufacturers, this type of direct communication can help organize questions before moving from initial material screening to ongoing procurement.


Industry exhibitions provide another opportunity to compare raw-material information directly with supplier representatives. At CHINACOAT 2026, visitors interested in rosin ester resins can discuss material options, documentation, physical forms, and sourcing arrangements with KOMO representatives. Such conversations can help procurement and technical teams identify the information they need for subsequent internal evaluation.


Professionals sourcing adhesive raw materials can meet the Komotac team at CHINACOAT 2026, November 11–13, 2026, China Import and Export Fair Complex, Guangzhou, Booth 5.2 C47. The discussion can focus on rosin ester grade selection, product documentation, packaging, and supply arrangements relevant to upcoming adhesive-material requirements.


0 comment
0 FacebookTwitterPinterestEmail

Initial low-cost quotes from overseas hardware vendors frequently mask severe financial liabilities that emerge only after shipping containers arrive at distribution hubs. Procurement teams often celebrate massive upfront savings without realizing that international logistics introduces complex pricing layers.


Unforeseen expenditures quickly erode initial budget margins, turning a seemingly economical transaction into an expensive operational burden for growing businesses.


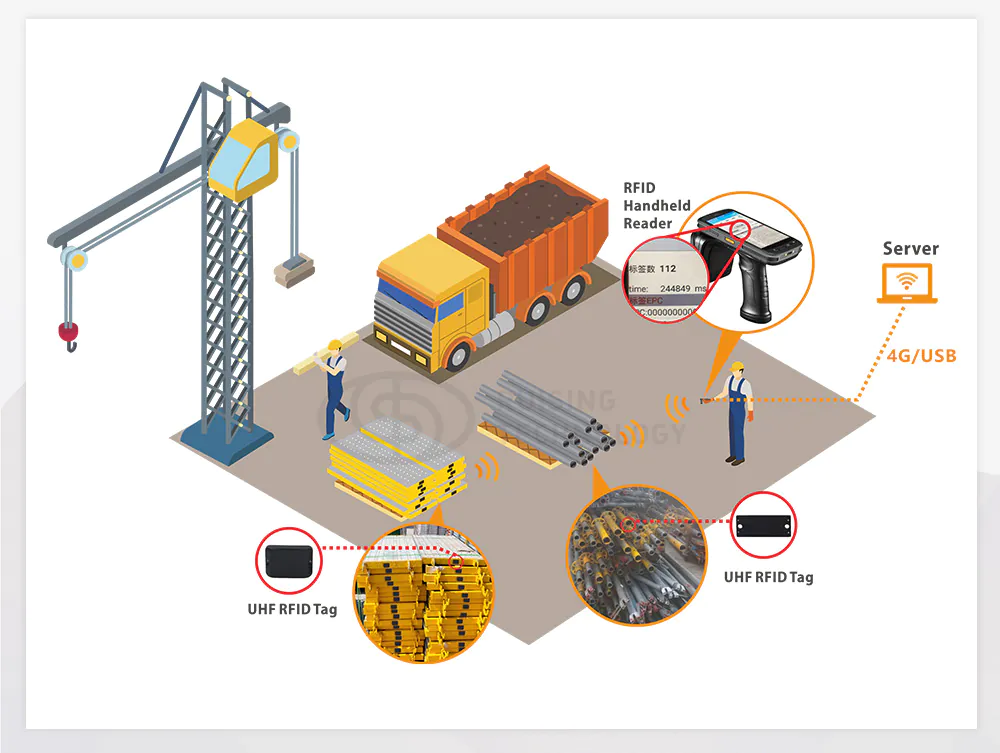
Calculations based solely on factory piece-rates fail to account for the true financial ecosystem governing international hardware procurement. Supply chain directors must evaluate every auxiliary expense before deciding to buy UHF RFID tags in bulk from distant manufacturing partners. Failing to uncover these hidden operational liabilities exposes corporate balance sheets to recurring financial shocks and unbudgeted cash outflows.


Sifting Through International Shipping Surcharges and Freight Volatility


Ocean freight rates fluctuate wildly based on fuel adjustments, geopolitical tensions, and seasonal port congestion patterns. Cargo carriers routinely impose unexpected terminal handling fees and emergency bunker surcharges upon arrival at destination ports. These shifting transport costs alter baseline budgets drastically before shipments ever clear customs inspection zones, leaving logistics managers facing severe financial deficits.


Dimensional weight calculations often penalize lightweight hardware shipments packed in oversized protective cartons. Freight forwarders bill based on volumetric space rather than actual gross mass, doubling expected shipping overhead unexpectedly. Managing these variables requires rigorous packing optimization that distant vendors rarely coordinate effectively for international clients.


Transit insurance premiums increase substantially when moving high-value tech inventory across international maritime routes. Unforeseen cargo damage claims involve lengthy investigation procedures that leave businesses without inventory or financial recourse for months. Sourcing partners must guarantee comprehensive transit coverage to protect capital investments during international shipping cycles.


Unbudgeted Tariffs, Customs Brokerage, and Compliance Fees


Import duties change abruptly following trade policy revisions or localized tariff adjustments imposed by regulatory agencies. Customs brokers charge substantial processing fees to clear shipments containing specialized radio frequency technology. Delays at border checkpoints accumulate costly daily storage penalties in port-adjacent warehouses while shipments await physical inspection.


Regulatory certification discrepancies can halt entire container loads indefinitely if documentation lacks required regional compliance markers. Securing local radio frequency approvals retroactively involves expensive third-party testing fees and prolonged operational downtime. Global suppliers sometimes ship uncertified hardware variants, leaving buyers legally and financially exposed.


Navigating complex tax compliance requirements across multiple international jurisdictions adds administrative overhead to every transaction. Bureaucratic red tape often delays port release dates, stalling downstream manufacturing and distribution schedules. Financial planners must budget for unexpected customs penalties to avoid severe cash flow interruptions.


Managing High Defect Rates and Quality Control Failures Abroad


Mass production facilities operating overseas sometimes compromise component soldering standards to hit aggressive price targets. Defective microchips or fractured internal antenna traces often go unnoticed until thousands of units enter active deployment. Scrapping faulty UHF RFID tags destroys profit margins instantly and halts active warehouse operations.


Returning defective inventory across international borders involves prohibitive return shipping costs and protracted customs clearance disputes. Foreign vendors frequently dispute failure claims, demanding exhaustive physical sample testing before issuing credit notes. Organizations absorb these losses directly when supplier warranty agreements lack enforceable legal protections.


Procurement teams can reduce project risk by working with suppliers that provide application testing, product customization, and technical support. RSTC offers these services for RFID projects.


The Financial Impact of Communication Incompatibilities and Middleware


Protocol variances between foreign hardware firmware and existing enterprise software architectures generate unexpected integration expenses. Custom middleware development becomes necessary when imported transponders utilize proprietary data formatting rules. Software engineers spend weeks writing translation scripts to bridge communication gaps between disparate systems without causing enterprise server crashes.


Incompatible operating frequencies or mismatched memory layouts render entire bulk orders completely useless within legacy warehouse management platforms. Remedying software misalignment demands costly external consulting hours that negate initial hardware purchase discounts. Enterprises must verify protocol harmonization thoroughly prior to committing capital expenditure.


Language barriers and time zone differences complicate technical troubleshooting when firmware bugs emerge during initial integration phases. Delayed communication loops extend software development cycles, pushing project deadlines back by several months. Such administrative friction silently drains valuable engineering resources from core business initiatives while increasing overall project risk profiles.


Total Landed Cost Analysis Versus Upfront Unit Savings


Comprehensive financial evaluations must encompass every operational variable from factory floor to final warehouse installation. Factoring in hidden transport surcharges, customs friction, defect allowances, and software adjustments reveals true acquisition costs. Organizations that choose to buy UHF RFID tags in bulk through verified channels avoid unexpected capital drain and maintain steady profitability.


Initial piece-rate quotes represent only a fraction of total lifecycle expenditures for international logistics projects. Industry leaders such as RSTC provide transparent pricing models that eliminate unexpected post-purchase financial liabilities completely. Detailed landed cost breakdowns allow corporate financial officers to allocate capital accurately without fearing sudden budget overruns.


Deploying high-performance UHF RFID tags through trusted manufacturing channels ensures long-term economic stability for enterprise supply chains. Strategic procurement oversight transforms international technology acquisition from a speculative gamble into a predictable operational asset. Organizations prioritizing complete visibility avoid the trap of illusory unit savings and protect their core profitability.


Working with an experienced RFID supplier can make technical requirements, testing, and project communication easier to define before procurement. Diligent oversight during supplier selection secures lasting operational efficiency and financial predictability.


0 comment
1 FacebookTwitterPinterestEmail